How to Choose Aluminum Tube Extrusions in 2026?

Choosing Aluminum Tube Extrusions in 2026 requires more than comparing price per kilogram. Engineers must examine alloy, temper, wall thickness, dimensional tolerance, surface finish, and joining requirements. A tube that looks economical may fail after bending, anodizing, or repeated thermal cycling. Small differences matter. A 0.5-millimeter wall variation can affect weight, pressure performance, and machining time.

Industry data shows why this decision deserves closer attention. The International Aluminium Institute reported global primary aluminum production above 72 million metric tonnes in 2024. Meanwhile, Grand View Research’s 2024 aluminum extrusion assessment forecasts continued market growth through the decade, driven by transportation, construction, renewable energy, and industrial equipment. These reports indicate strong demand, but they do not identify the best profile for every application. That part still requires engineering judgment.

Charles M. “Chuck” Johnson, former president and chief executive of The Aluminum Association, has stated, “Aluminum is infinitely recyclable.” His point supports a practical evaluation of recycled content, traceability, and end-of-life recovery. Yet recyclability alone should not decide the purchase. Alloy 6061 may suit strength-focused frames, while 6063 often offers better extrusion detail and surface appearance. The correct answer depends on loading, environment, tolerances, and production volume. This guide will not pretend that one alloy wins everywhere. Supplier capability can vary, and published market figures may use different definitions. Careful sampling, inspection reports, and prototype testing remain essential before approving production.

How to Choose Aluminum Tube Extrusions in 2026?

Define the Application Requirements for Aluminum Tube Extrusions

How to Choose Aluminum Tube Extrusions in 2026?

Define the Application Requirements for Aluminum Tube Extrusions

Start with the real working conditions, not a catalog shape. Identify the tube’s purpose, expected load, span, and movement. A square tube may suit a rigid frame, while a round tube often handles rotation and fluid flow more effectively. Record the outside dimensions, wall thickness, and allowable tolerance. Measure twice.

Temperature, moisture, chemicals, and ultraviolet exposure can change the selection. Outdoor equipment may need corrosion-resistant alloy and a suitable surface treatment. Indoor assemblies still require protection near cleaning agents or condensation. Do not assume a thicker wall always solves the problem. It can add unnecessary weight and affect assembly.

Review how the extrusion will be cut, drilled, bent, joined, and inspected. Specify the required temper because strength and formability can conflict. Check whether fasteners, welds, or inserts create local stress around the tube. I once focused only on static load, and vibration later caused loosened joints. That shortcut failed.

Ask for dimensional data, mechanical properties, and test documentation from a qualified supplier. Compare tolerances with the mating parts, especially when seals, sliding components, or automated fixtures are involved. Define the acceptable finish, straightness, and length variation before ordering. Small gaps can become expensive rework. A prototype can reveal problems that calculations miss.

Compare Aluminum Alloys, Tempers, and Mechanical Properties

How to Choose Aluminum Tube Extrusions in 2026?

Alloy selection starts with the load, not the catalogue. According to Aluminum Standards and Data 2024, 6063-T5 typically provides about 145 MPa yield strength and 186 MPa tensile strength. It extrudes smoothly and gives clean surfaces for architectural tubes. For heavier frames, 6061-T6 commonly reaches about 240 MPa yield strength and 290 MPa tensile strength. The trade-off is real. Its lower extrudability can increase cost and corner distortion.

Temper changes performance without changing the alloy family. T5 means cooling after extrusion, followed by artificial aging. T6 requires solution heat treatment and artificial aging. This usually raises strength, but may increase distortion or reduce dimensional stability. ASTM B221 specifies requirements for aluminum alloy extruded tubes, including tensile testing and dimensional control. Always request a mill test report. Published values are not promises.

Wall thickness matters too. A 2-millimeter tube may meet a strength target, yet buckle under compression or vibration. I have seen designs fail because engineers compared tensile strength alone. Check yield strength, elongation, fatigue exposure, and weld-zone softening. For welded 6061-T6 assemblies, the heat-affected area can lose much of its original temper strength. Use verified data from Aluminum Standards and Data 2024, ASTM B221, and the supplier’s lot certificate. Allowance for variation is wise.

How to Choose Aluminum Tube Extrusions in 2026?

Compare common extrusion alloys and tempers by representative tensile and yield strength values.

7075-T6 provides the highest strength among these options, while 6063-T5 offers lower strength with good extrudability and surface finishing characteristics. 6061-T6 and 6082-T6 provide balanced strength for structural tube applications. Values shown are representative minimum properties for common wrought aluminum products and may vary according to the applicable standard, wall thickness, section size, and temper.

Choose Tube Shapes, Dimensions, Wall Thickness, and Tolerances

How to Choose Aluminum Tube Extrusions in 2026?

Choose Tube Shapes, Dimensions, Wall Thickness, and Tolerances

Start with function. A square tube suits frames that need flat mounting faces and simple corner joints. Round tubes work well for handrails, fluid paths, and rotating components. Rectangular tubes can improve bending resistance in one direction. In practical design reviews, shape often affects assembly time more than expected. Consider access for fasteners, drainage, welding, and surface finishing before selecting a profile.

Define outside dimensions and inside clearance together. A 40 × 20 mm rectangular tube may fit a compact frame, but internal space can disappear after coating or joining. Wall thickness should reflect load, span, buckling risk, and machining requirements. Thin walls reduce weight. They can also deform during clamping. For a lightly loaded enclosure, a thin wall may be reasonable. For a structural support, confirm calculations and test assumptions. My first estimate is not always right.

Tolerances deserve equal attention. Request clear limits for outside dimensions, wall thickness, straightness, twist, and cut length. Tight tolerances can increase cost without improving performance. Loose tolerances may create visible gaps or difficult assemblies. Build a tolerance stack-up around the complete product, not one tube alone. Check the latest drawings with the extruder before production. A small radius change can alter strength, tooling, and fit. Prototype one section when the design has little adjustment room.

Assess Surface Finishes, Fabrication Needs, and Standards

How to Choose Aluminum Tube Extrusions in 2026?

Surface finish affects appearance, maintenance, and service life. Choose anodizing when you need a hard, uniform surface for indoor or outdoor use. Powder coating offers broader color choices and can hide minor extrusion marks. Mill finish costs less, but it may show scratches, oxidation, and handling stains. Request a sample section before approving production. A digital color image is not enough.

Fabrication requirements should guide the tube design. Confirm cutting tolerances, hole locations, bending radius, and weld access early. Thin walls reduce weight, but they can deform during drilling or clamping. I have seen attractive profiles fail because fasteners crushed the tube edge. Allow space for inserts, internal supports, or drainage paths. Small details matter.

Standards provide a dependable technical baseline. Check alloy, temper, dimensional tolerances, coating thickness, and mechanical properties in the supplier’s documentation. For structural applications, review the applicable regional building and safety requirements. Ask for inspection records and material traceability. Standards change, and older drawings can contain outdated references. Verify the current edition before production. Do not assume a familiar specification fits every application. Evaluate corrosion exposure, load conditions, joining methods, and expected maintenance together. Testing one finished assembly is wiser than trusting a profile table alone.

Evaluate Suppliers, Costs, Lead Times, and Quality Control

How to Choose Aluminum Tube Extrusions in 2026?

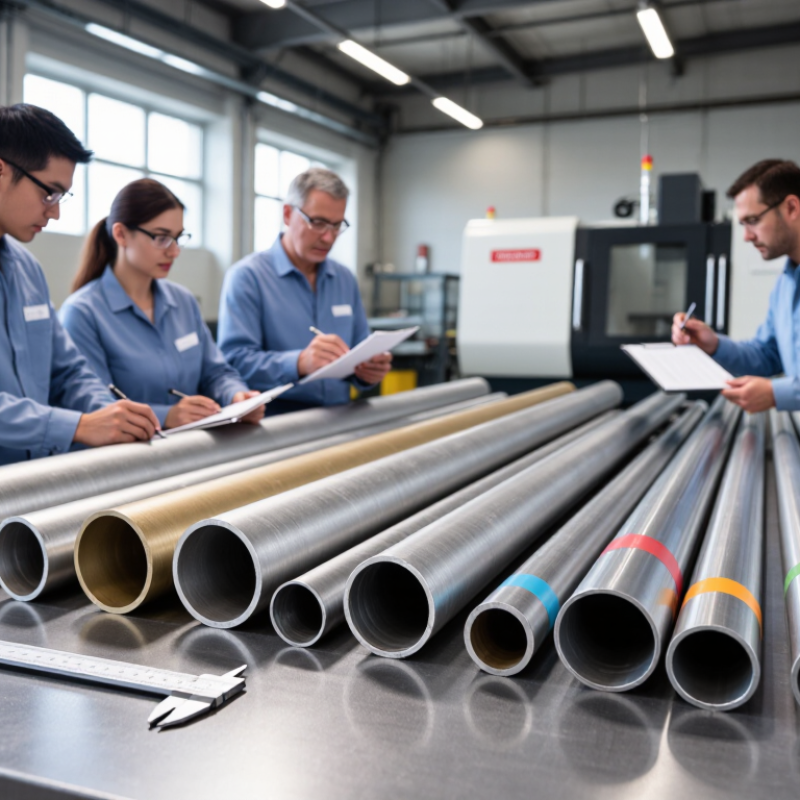
Choosing aluminum tube extrusions requires more than comparing prices on a spreadsheet. Supplier capability matters. Request production samples, tolerance charts, alloy details, and recent quality records before placing an order. A reliable supplier should explain die design, extrusion limits, surface treatment, and inspection methods clearly. Ask whether inspectors check wall thickness, straightness, dimensions, and surface marks during production.

Costs often change after quoting. Tooling, packaging, cutting, finishing, testing, and freight may appear separately. Compare the complete landed cost, not only the price per kilogram. Lead time also needs careful review. Confirm die preparation, first-article approval, production capacity, and shipping schedules in writing. A supplier promising ten days may exclude tooling or inspection time. That happens.

Tips: Order a small trial batch. Measure several tubes with calibrated tools. Check the certificate against the delivered alloy. Photograph packaging damage immediately. Keep one approved sample for future comparisons. Do not rely on appearance alone.

Quality control should match the tube’s real use. Structural applications need tighter dimensional control and traceable test results. Decorative parts may require stronger surface inspection. Ask how nonconforming material is isolated and corrected. My experience is that clear inspection plans prevent more problems than urgent complaints. Still, plans can fail when specifications are vague. Review them with the supplier before production begins, and revise weak points openly.

How to Choose Aluminum Tube Extrusions in 2026? — Evaluate Suppliers, Costs, Lead Times, and Quality Control
Evaluation Dimension Specification / Data Point Typical 2026 Planning Range Preferred Target Why It Matters Recommended Verification
Alloy Selection 6063-T5 / 6063-T6 Yield strength commonly about 145–214 MPa, depending on temper and wall thickness Use for architectural, enclosure, heat-transfer, and general-purpose tubing Offers good extrudability, surface finish, corrosion resistance, and availability Review the mill test certificate and confirm compliance with ASTM B221 or an equivalent regional standard
Alloy Selection 6061-T6 Yield strength commonly about 240 MPa or higher for many standard product forms Use when higher structural strength and machinability are required Usually stronger than 6063, but generally more difficult to extrude and finish Confirm temper, mechanical properties, chemical composition, and minimum wall capability
Alloy Selection 6005A-T6 or similar structural alloy Yield strength commonly about 225–250 MPa, subject to product form and specification Use for structural tubes where strength-to-weight performance is important Can provide a practical balance between strength, extrudability, and corrosion resistance Request certified tensile-test results for the actual production lot
Dimensional Capability Outside diameter and wall thickness Common commercial tube sizes: approximately 10–150 mm outside diameter; wall thickness around 1–8 mm Select the smallest wall that meets strength, stiffness, forming, and machining requirements Wall thickness strongly affects weight, cost, die difficulty, and minimum-order quantity Compare supplier tolerances with ASTM B221, EN 755, or the drawing tolerance specified in the purchase order
Profile Complexity Hollow ratio, ports, ribs, and tight corners Simple round or rectangular tubes generally have lower tooling risk than multi-void or thin-wall profiles Use a simple cross-section unless the added geometry delivers measurable product value Complex dies can increase tooling cost, trial iterations, scrap, and lead time Request a die-feasibility review, extrusion-ratio assessment, and sample-section analysis
Raw Material Cost Aluminum billet and conversion content Budget using an aluminum index or billet surcharge plus conversion; finished extrusion pricing often varies by alloy, size, and quantity Require a transparent formula separating metal price, conversion charge, finishing, packaging, and freight Aluminum market movement can materially change quoted prices between order and shipment Ask for the price basis, index date, surcharge mechanism, and validity period of the quotation
Conversion Cost Extrusion conversion charge Indicatively about USD 1.00–3.50 per kg for standard profiles; complex or low-volume profiles may be higher Compare quotes only after normalizing alloy, profile weight, length, finish, quantity, and packaging Conversion charges reflect press size, die complexity, production yield, labor, and energy Request a line-item quotation and confirm whether die trials, cutting, inspection, and packing are included
Tooling Cost Extrusion die and trial charges Simple dies may be approximately USD 300–1,500; complex hollow or multi-port dies may exceed USD 3,000 Obtain ownership, maintenance, storage, and replacement terms in writing Die cost is usually a one-time expense but can be significant for low-volume projects Confirm die life assumptions, trial quantity, revision policy, and whether the die remains dedicated to the buyer
Surface Finish Mill finish, anodizing, powder coating, or mechanical finishing Typical added lead time: 5–15 working days, depending on finish, color, batch size, and inspection requirements Specify finish type, color reference, gloss, film thickness, and visible-surface requirements Finishing can affect appearance, corrosion resistance, dimensional fit, and total cost Approve a physical master sample and define acceptable color, gloss, coating thickness, and surface defects
Minimum Order Quantity Commercial production quantity Common starting quantities range from approximately 300–1,000 kg per profile; custom terms vary Match the order size to die amortization, finish batch size, and annual demand Small orders usually carry higher conversion, setup, finishing, and freight costs per kilogram Request price breaks at sample, pilot, 1-ton, 5-ton, and annual-contract volumes
Sample Lead Time First extrusion samples after drawing approval Approximately 2–5 weeks for a standard profile; 4–8 weeks for complex tooling or multiple revisions Obtain dimensional samples before approving mass production Early sampling reduces the risk of discovering die, fit, or finish problems after production Use a signed drawing, inspection plan, sample approval record, and change-control process
Mass-Production Lead Time Extrusion only Approximately 3–6 weeks after order, material, drawing, and die approval Build a schedule with production, inspection, packing, and dispatch milestones Lead time depends on press availability, billet allocation, die readiness, and order quantity Ask for a written production schedule and a defined late-delivery escalation process
Finished-Goods Lead Time Extrusion plus anodizing or powder coating Approximately 5–9 weeks after all technical approvals; special colors or secondary operations may add time Allow additional contingency for first production and external finishing capacity Multiple process steps create additional scheduling and quality-control interfaces Require process-by-process status updates and a final pre-shipment inspection date
Supplier Capacity Press size, monthly capacity, and backup production capability Small, medium, and large presses differ substantially in billet diameter, maximum profile size, and available tonnage Select a press that can produce the profile without excessive extrusion ratio or scrap Capacity and press suitability affect dimensional stability, productivity, and delivery reliability Request equipment list, relevant profile references, capacity statement, and planned production location
Quality System Manufacturing and inspection management ISO 9001 certification is a useful baseline; product-specific control plans remain necessary Supplier maintains documented incoming, in-process, final, and nonconformance controls A certificate alone does not prove that the actual profile will meet the drawing Audit the certificate scope, inspection records, calibration system, corrective-action process, and traceability
Dimensional Inspection Outside dimensions, wall thickness, straightness, twist, length, and cut quality Use drawing tolerances or applicable standards; critical fits may require tighter, separately agreed tolerances 100% inspection for critical dimensions during first article; sampling after process capability is demonstrated Extrusion dimensions can vary with temperature, die wear, cooling, stretching, and cutting Review first-article inspection reports, calibrated instruments, CMM records, and capability data where applicable
Mechanical Testing Tensile strength, yield strength, elongation, and hardness Requirements depend on alloy, temper, wall thickness, and governing standard Every production lot is traceable to a material certificate and, where specified, test results Correct alloy designation does not guarantee the required temper or mechanical performance Review certified test results and verify sampling frequency, test method, and lot traceability
Surface Quality Scratches, die lines, dents, discoloration, pits, weld lines, and coating defects Acceptance depends on viewing distance, visible surface, finish type, and agreed reference samples Define cosmetic zones and defect limits before production Visual acceptance can be subjective if the purchase specification is incomplete Use approved limit samples, controlled lighting, inspection distance, and documented defect criteria
Traceability Billet, heat, extrusion lot, finish batch, and packing identification Each shipment should link finished bundles to production and material records Maintain traceability from raw material through shipment Traceability enables faster root-cause analysis and targeted containment if a defect occurs Check bundle labels, heat numbers, certificates, inspection reports, and packing-list consistency
Logistics Cost Packaging, inland transport, freight, insurance, and import charges Long-length aluminum products can incur non-standard freight or dimensional surcharges Compare total landed cost rather than ex-works or unit price alone Freight and packaging can materially change the economics of low-density or long-length products Request quotations under the same Incoterm, destination, length, bundle weight, and insurance assumptions
Commercial Risk Payment terms, price validity, claim handling, and delivery performance Common structures include deposit plus balance against shipment documents; terms vary by supplier and risk level Use milestone payments linked to sample approval, production completion, and inspection Commercial controls reduce exposure to late delivery, nonconforming goods, and unexpected surcharges Include acceptance criteria, replacement or credit terms, response time, and documented change approval in the contract
Planning note: Cost, capacity, tolerances, and lead-time figures are indicative industry benchmarks for 2026 budgeting. Final values should be confirmed against the selected alloy, profile drawing, order quantity, surface finish, delivery destination, applicable standard, and supplier quotation.
Shopping Cart
Scroll to Top

Search for...

The Duravant family of operating companies serve the food processing, packaging and material handling segments.