Top 10 Car Wiring Harness Duct Machines for Buyers in 2026
As vehicle platforms grow more complex, the equipment used to form and process protective ducts deserves closer attention. The Car Wiring Harness Duct Machine sits at a practical point in production: its accuracy can affect duct fit, routing consistency, and downstream assembly. Small variations matter. A poorly matched duct may create rework around clips, bends, or crowded dashboard areas.
The International Energy Agency’s Global EV Outlook 2025 reports that electric-car sales exceeded 17 million in 2024, representing more than one-fifth of global car sales. OICA’s 2024 production statistics also show the continued scale of global vehicle manufacturing. These reports describe market activity, not machine demand directly. Still, they help explain why buyers are assessing flexible equipment for changing vehicle programs and production volumes.
This Top 10 guide compares machines through buyer-focused criteria: duct size range, forming consistency, changeover time, controls, safety features, service access, and supplier support. A specification sheet can look convincing. Real production is less tidy. Material variation, operator experience, and line layout can all affect results, so no single machine is best for every factory. The models below are intended to help buyers ask sharper questions before requesting trials, references, or a quotation.
What Car Wiring Harness Duct Machines Do and How They Work
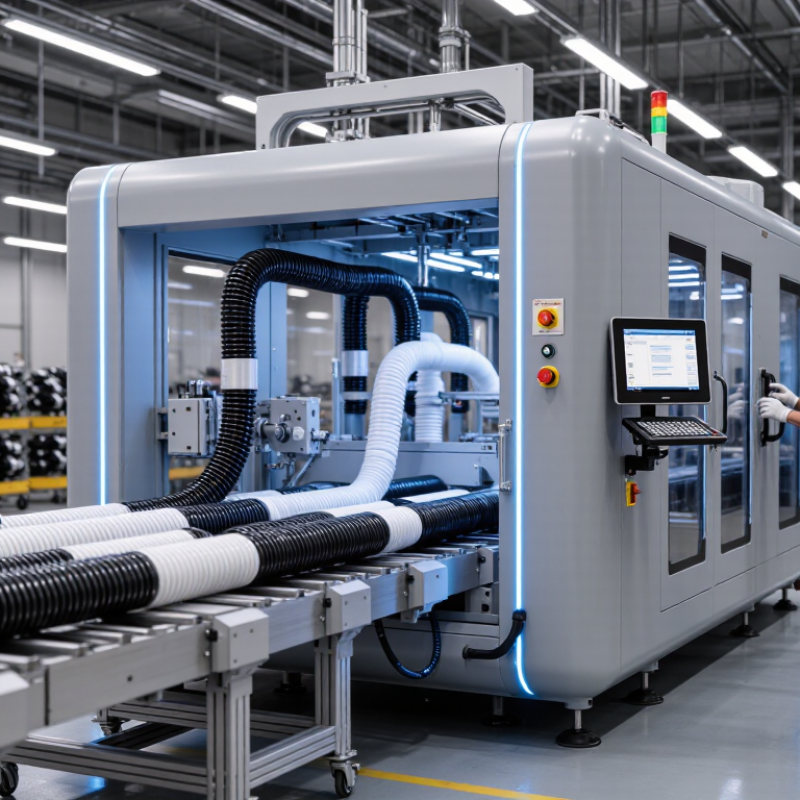
A car wiring harness duct machine prepares protective channels that guide and separate vehicle wiring. Depending on the production line, it may feed plastic duct from a coil or accept straight lengths, then measure and cut each piece. Some machines also punch openings or trim edges to match a specified layout.
That matters. Clean cuts help duct sections fit together without sharp plastic fragments near the wires.
During operation, feed rollers move the material past a length sensor. A guarded cutting blade stops it at the programmed measurement. If openings are needed, a punch unit makes them at set positions. Operators typically check the first few pieces with a ruler or profile gauge, then inspect samples as production continues.
Small errors add up. A worn blade can leave rough edges, while loose guides may shift a slot by a few millimeters.
Real setups are not always tidy. Different duct profiles can need separate guides, cutting settings, and test runs. A practical machine choice depends on material, duct size, required cut accuracy, and daily output—not just speed.
Even a capable system needs regular checks for blade wear, sensor alignment, and plastic debris around the feed path.
Key Machine Types Used in Automotive Duct Production
Automotive duct production relies on several machine types, not one universal line. Corrugated-tube extrusion lines melt polymer, form ribs in a rotating mould, and cool the duct. They suit flexible protection routes around tight engine-bay bends. Rigid duct systems may instead use profile extrusion, followed by cutting and end-forming. Small differences matter.
Cutting and slotting machines create repeatable lengths, openings, and branch points. End-forming stations flare or shape duct ends for clips and connectors. Automated feeding and assembly equipment can add clips, seals, or covers. Inspection stations check dimensions, wall consistency, and cut quality. Buyers should verify that samples match actual harness routes, not just catalogue dimensions.
OICA recorded 93,546,599 motor vehicles produced worldwide in 2023, about 10% more than in 2022, in its 2024 production statistics. The IEA’s Global EV Outlook 2024 reported nearly 14 million electric-car sales in 2023. These figures show the scale and changing mix of vehicle production; they do not directly predict duct-machine demand. For buyers, compare changeover time, material range, scrap rate, and measurable output. A fast line can still be the wrong choice. The awkward part is often tooling.
How to Compare Machines for Performance, Precision, and Cost
When comparing car wiring harness duct machines in 2026, test them with the duct material and geometry your line actually uses. A fast demonstration is not enough. Record cycle time across repeated runs, including feeding, forming, cutting, and changeovers. Note jams and operator adjustments, too. A machine that performs well only with one easy profile may slow production later.
Precision needs evidence from finished parts. Check cut length, bend consistency, edge quality, and fit against the harness layout. Run samples at different speeds and after a normal production shift. Small errors can accumulate. Ask how calibration works and which measurements the machine records. Supplier specifications help, but your own test results matter more.
Cost is more than the purchase price. Include tooling, installation, energy use, maintenance, spare parts, and operator training. Then compare the cost per acceptable part, not just the quoted machine price. Service response time matters when a line stops. I would also question optimistic output estimates; real changeovers are rarely as smooth as a showroom demo. A lower-cost machine may still be the better choice if it meets your tolerances and fits your production volume.
Top 10 Car Wiring Harness Duct Machine Comparison Criteria for 2026
Suggested evaluation weights for comparing machine performance, precision, and cost. These are planning guidelines, not measured scores for specific machines.
Use the same duct materials, part geometry, and production conditions when requesting cycle-time, accuracy, changeover, and scrap data from suppliers. Verify safety and service requirements against your facility’s needs.
Top 10 Car Wiring Harness Duct Machines for Buyers in 2026
For buyers in 2026, the most useful car wiring harness duct machines depend on duct material, shape, and daily output. A practical shortlist includes extrusion lines, corrugation formers, automatic cutters, slotting machines, end-flaring units, and heat-shaping stations. Each handles a different production task. Check whether the equipment supports your duct’s wall thickness and bend radius, not just its advertised speed.
Other useful options include clip-insertion machines, print-marking systems, vision inspection stations, and automatic packing equipment. Together, these ten machine types can support a line from raw polymer to checked, labeled duct sections. Ask suppliers to run your actual material through a sample setup. Look closely at cut edges, slot spacing, and deformation after bending.
Small defects matter.
A neat ranking can mislead. A compact shop may need reliable cutting and inspection before automation for every step. Compare changeover time, spare-part access, guarding, and operator training. Request measured cycle times across several duct sizes, not one ideal sample. Also inspect scrap rates during startup; this figure is often overlooked. Some specifications look excellent on paper, yet require more adjustment than expected.
How to Select a Machine for Your Production Requirements
Choosing a car wiring harness duct machine starts with the part, not the catalogue. List duct material, diameter, wall thickness, bend radius, cut length, and daily volume. Check whether one machine handles your full range without manual retooling. Ask for cycle-time measurements using your actual duct, including feeding, heating, cooling, and unloading. A fast forming cycle can still lose hours through frequent changeovers. Check fit. Test changeovers. Confirm how sensors detect a missed feed or incomplete bend.
Production plans matter too. The International Federation of Robotics’ World Robotics 2024 report counted 4.28 million industrial robots operating worldwide in 2023. This reflects automation’s broad manufacturing role, though it is not a forecast for harness equipment. Evaluate machine interfaces, guarding, traceability, and integration with cutting and assembly stations. Compare uptime commitments, service response, spare-part lead times, energy use, and operator training—not only output claims. Request sample parts and inspect dimensions, surface marks, and scrap across several shifts. I would still insist on a production trial; specification sheets can look cleaner than a real line. A flexible machine may cost more or run slower on one fixed product. Choose for your product mix and bottleneck, and document acceptance limits before purchase.
Top 10 Car Wiring Harness Duct Machines for Buyers in 2026 - How to Select a Machine for Your Production Requirements
This is a process-based comparison, not a ranking of specific models or suppliers. Capacity figures are indicative planning ranges for common industrial setups; actual output depends on duct material, dimensions, cut length, tooling, automation, and quality requirements. Confirm specifications and acceptance criteria with each supplier.
| Rank | Machine Type | Typical Process and Materials | Indicative Production Range | Typical Capability to Specify | Best Suited For | Key Selection Checks |
|---|---|---|---|---|---|---|
| 1 | Corrugated Conduit Cut-to-Length Machine | Feeds and cuts corrugated plastic conduit, commonly used to protect automotive wire bundles. | About 300–1,500 cuts/hour, depending on tube diameter, cut length, and feeding method. | Tube diameter range, cut-length range, length tolerance, blade type, and recipe storage. | High-volume production of repeatable conduit segments. | Test the actual conduit material and corrugation profile; check for crushed ends, burrs, and cut-length consistency. |
| 2 | Corrugated Conduit Cutting and Slitting Machine | Cuts conduit to length and makes a longitudinal slit for installation over an existing harness. | About 200–1,000 pieces/hour; output varies with length, diameter, and slit configuration. | Slit depth and position, supported tube sizes, cut-length tolerance, and changeover time. | Harness programs that require split loom or openable protective conduit. | Verify that the slit remains continuous without weakening the tube or creating sharp edges; trial the full range of tube sizes. |
| 3 | Corrugated Tube End-Forming Machine | Forms, flares, or shapes conduit ends to support connector, grommet, or fitting assembly. | About 200–800 ends/hour, depending on whether one or both ends are processed per cycle. | Tooling range, end-form geometry, heating or forming method, and repeatability. | Applications that need a shaped end for assembly or improved component retention. | Check material compatibility, end geometry, cycle time, and whether formed ends pass the required fit and pull tests. |
| 4 | Rigid Plastic Wiring Duct Extrusion Line | Extrudes rigid plastic wiring duct profiles, including slotted duct used for routing and organizing wires. | Line speed is commonly specified in metres/minute; practical output depends on profile, wall thickness, cooling, and downstream cutting. | Profile dimensions, material formulation, screw and die design, cooling capacity, and haul-off control. | Manufacturers producing rigid duct profiles in-house rather than purchasing finished lengths. | Review the full line layout, die capability, dimensional stability, material requirements, and tooling costs before comparing line speeds. |
| 5 | Rigid Duct Cut-to-Length Saw | Cuts extruded rigid duct profiles to specified lengths using a saw or flying-cut system. | About 100–600 lengths/hour, depending on profile size, cut length, and bundling requirements. | Maximum profile dimensions, cut-length tolerance, blade selection, and dust or chip control. | Processors converting rigid duct extrusion into finished stock lengths. | Check squareness, edge quality, profile support, chip extraction, and compatibility with the extrusion line’s output speed. |
| 6 | Rigid Duct Slotting and Punching Machine | Creates slots, holes, or other specified openings in rigid plastic duct and covers. | About 100–500 pieces/hour; tooling pattern and number of operations strongly affect output. | Slot pitch, opening dimensions, profile support, tool life, and registration accuracy. | Production of slotted wiring duct or custom duct sections. | Confirm the drawing-based feature layout, repeatability over the full part length, burr control, and ease of tooling replacement. |
| 7 | Braided Sleeve Hot-Knife Cutting Machine | Feeds and heat-cuts braided protective sleeve to reduce fraying at the cut ends. | About 200–1,000 cuts/hour, depending on sleeve diameter, cut length, and handling requirements. | Supported sleeve materials and diameters, cut-length range, temperature control, and fume extraction. | Harness operations using braided sleeves or other fray-prone protective coverings. | Validate the edge condition and thermal effect on the specific sleeve; assess ventilation and operator protection needs. |
| 8 | Heat-Shrink Tubing Cut-to-Length Machine | Measures and cuts heat-shrink tubing used for harness protection, insulation, or joint covering. | About 300–1,500 cuts/hour, depending on tubing size, length, and feed arrangement. | Tube diameter, wall thickness, cut-length tolerance, feed accuracy, and recipe changeover. | Repeatable preparation of heat-shrink pieces before harness assembly. | Test actual tubing for feeding slip, deformation, and edge quality; confirm length accuracy at both short and long cut settings. |
| 9 | Harness Conduit Feeding and Insertion Machine | Feeds protective conduit and assists with positioning or inserting it over wire bundles or harness sections. | About 60–300 assemblies/hour, depending on harness length, branching, and manual loading. | Harness length range, conduit diameter, feed force, fixture flexibility, and changeover requirements. | Assembly cells with recurring harness layouts and substantial conduit-handling work. | Run trials with representative harnesses, including branches and connectors; check for wire damage, snagging, and fixture access. |
| 10 | Harness Tape Wrapping Machine | Applies protective tape around harness sections, often alongside conduit or sleeve processes. | About 30–200 harnesses/hour, depending on wrap length, overlap, branching, and operator involvement. | Tape width and overlap control, wrap tension, supported harness geometry, and program storage. | Harness lines where protective wrapping is combined with duct and sleeve installation. | Check tape tension and overlap consistency, access around branches, changeover time, and compatibility with the specified tape. |